
Gas Assist Injection Molding: Process, Benefits and Design
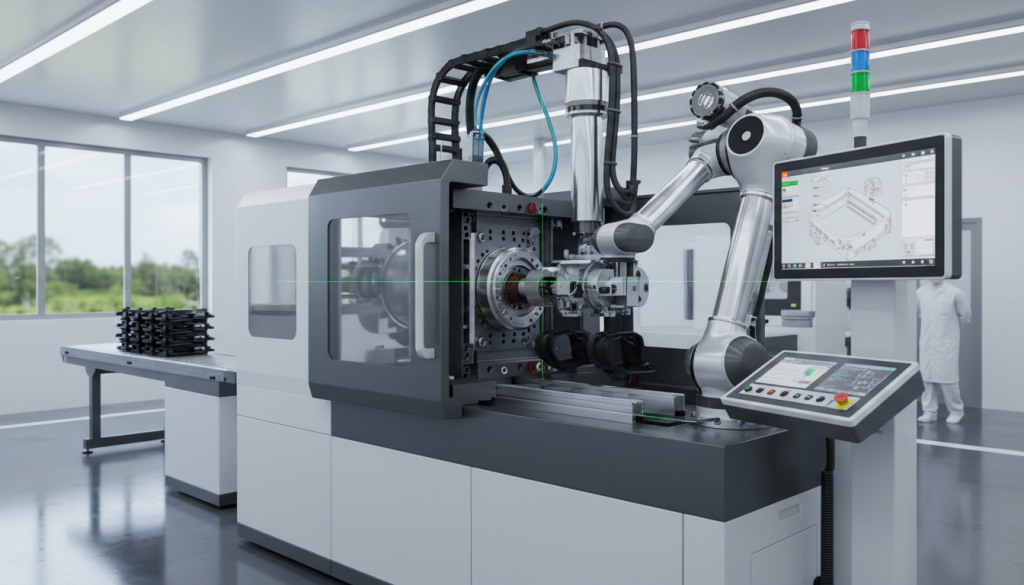
Gas assist injection molding is a specialized low-pressure manufacturing process where pressurized nitrogen gas is injected into a mold to create hollow sections within a plastic part. Are you currently facing challenges with heavy components that drive up material costs or surface defects that compromise your brand’s aesthetic? Traditional molding methods often struggle with thick-walled designs, leading to unsightly sink marks and internal stresses that cause warping. By implementing gas assist injection molding , the process may reduce mass or sink risk in suitable geometries, subject to gas-channel design, resin behavior and validation.
What is gas assist injection molding in manufacturing?
How does the gas assist process work?
The process works by injecting a “short shot” of resin into the mold followed by high-pressure nitrogen to fill the cavity. This gas flows through pre-designed channels to displace material in thick areas and press the resin against the mold walls.
Here is the thing.
- Nitrogen gas displaces molten plastic.
- Hollow sections are formed internally.
- Pressure is maintained during cooling.
| Feature | Description | |
|---|---|---|
| Media Used | Pressurized Nitrogen Gas | |
| Pressure Level | Lower than conventional molding | |
| Core Structure | Hollowed internal channels |
Key Takeaway: Gas assist utilizes the path of least resistance to create hollow structures that maintain external dimensions without the weight of solid plastic.
Our analysis shows that this technique effectively bridges the gap between lightweight design and structural integrity for small and medium housings.
How does internal gas assist injection molding function?
How is nitrogen distributed inside the mold?
Internal gas assist injection molding functions by introducing gas into the center of the molten resin stream through specialized nozzles. This creates a continuous gas bubble that pushes the molten skin toward the cavity surface while the channel develops; final geometry still depends on tool, material and process control.
Believe it or not.
- Gas enters through the nozzle or runner.
- It stays contained within the plastic walls.
- Pressure remains constant during solidification.
| Component | Internal Gas Assist Role | |
|---|---|---|
| Nitrogen | Forms the hollow core | |
| Resin | Forms the exterior skin | |
| Mold Walls | Defines the final part shape |
Key Takeaway: Internal gas assist is the primary method for creating high-strength, hollow-ribbed parts while reducing raw material consumption.
The internal pressure prevents the part from shrinking away from the mold, which can help manage shrinkage in suitable geometries; dimensional stability still requires drawing-based validation.
Why choose external gas assist injection molding for parts?
How does external gas assist improve surfaces?
External gas assist is used to press the front surface of a part against the mold by injecting gas between the back surface and the core. This can improve support of the cosmetic surface, but texture replication, rib read-through and other appearance criteria must be validated on the actual part.
You might be wondering.
- Gas acts as a pressure cushion.
- It packs the resin from the reverse side.
- No gas enters the actual plastic material.
| Benefit | External Gas Assist Impact | |
|---|---|---|
| Surface Finish | May reduce sink risk | |
| Texture | Validate texture replication | |
| Internal Stress | Significant reduction in warping |
Key Takeaway: External gas assist is one option for appearance-sensitive panels when the geometry, gas seal and surface acceptance plan support it.
By applying pressure to the back of the part, you can maintain thick supporting structures without compromising the cosmetic integrity of the visible surface.
What are the cost benefits of gas assist injection molding?
How does this method reduce tooling expenses?
Gas-assisted molding reduces costs by requiring significantly lower clamping forces, which allows for the use of more affordable injection molds . Lower tonnage machines can often be used for the same part, directly decreasing your hourly production rates and capital investment.
But wait, there’s more.
- Reduced material usage lowers unit costs.
- Lower clamping force extends tool life.
- Freight costs drop due to lighter parts.
| Cost Driver | Potential project effect | |
|---|---|---|
| Material | Lower resin use in suitable channels | |
| Tooling | Lower maintenance requirements | |
| Logistics | Reduced shipping weight |
Key Takeaway: The combination of material savings and lower equipment requirements makes gas assist one of the most cost-efficient processes for thick-section plastic parts.
Financial optimization is achieved not just through manufacturing speed, but through the holistic reduction of material and energy inputs.
Which design advantages does gas assist injection molding offer?
How does gas assist enable complex designs?
This technology enables designers to incorporate varying wall thicknesses and hollow ribs into a single, unified component. You can consolidate multiple parts into one, reducing the need for fasteners, adhesives, and labor-intensive assembly.
Make no mistake.
- Thick and thin sections coexist.
- Ribs can be placed without sink marks.
- Internal gas channels act as reinforcements.
| Design Element | Gas Assist Advantage | |
|---|---|---|
| Part Consolidation | Reduces assembly bill of materials | |
| Wall Thickness | Allows for thick structural ribs | |
| Dimensional Stability | Holds tight tolerances over long spans |
Key Takeaway: Design for gas assist when the channel path, strength, appearance and business case compare favorably with conventional molding or other routes.
Integrating structural support directly into the part geometry removes the secondary costs often associated with reinforcement.
Can you convert metal parts to gas assist injection molding?
Why is gas assist a metal replacement solution?
Gas-assisted molding can be evaluated as an alternative to some metal enclosures or structures. Material properties, loads, temperature, fire performance, finish and any remaining secondary operations must be compared for the application.
Check this out.
- Plastic is naturally corrosion-proof.
- Molded-in color removes painting steps.
- Complex shapes are molded in seconds.
| Property | Gas Assist Plastic vs. Metal | |
|---|---|---|
| Weight | Significant reduction in mass | |
| Corrosion | Depends on resin and environment | |
| Secondary Ops | May change secondary operations |
Key Takeaway: Gas assist can be evaluated for automotive, medical and other applications only after the material, load, appearance and regulatory requirements are defined.
Any return-on-investment case should compare tooling, material, cycle, labor, secondary operations, quality and expected volume using project data.
Which small and medium parts benefit from gas assist injection molding?
Where does gas assist help most?
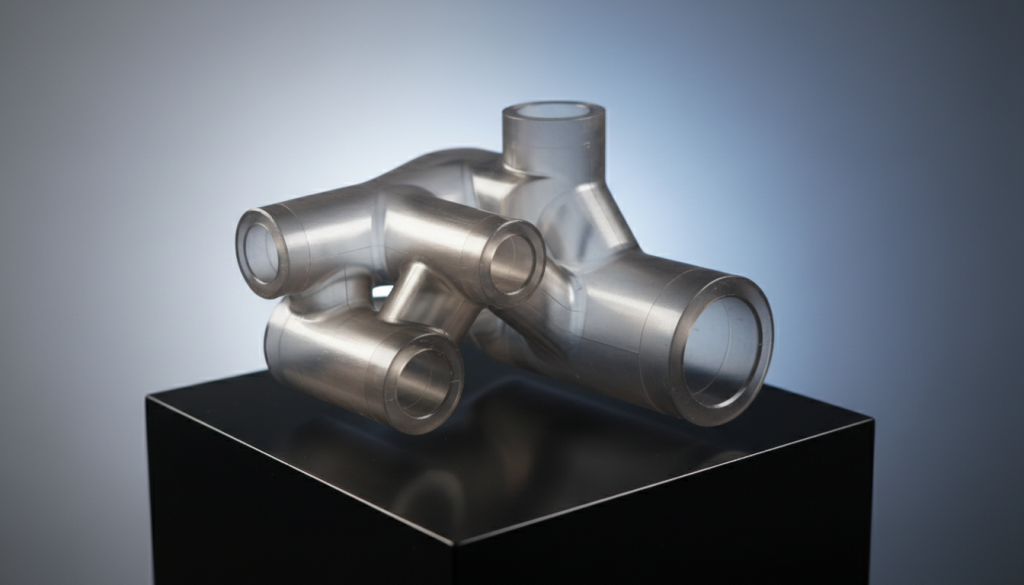
Gas assist is most useful on parts with thick sections that would otherwise sink or warp, such as handles, grips, thick ribs, tubular sections and bosses on small and medium housings. The gas cores out the thick area, so the part is lighter and flatter without a long hold time.
- Hollow handles and grips stay light and stiff.
- Thick ribs and bosses show less sink on the visible face.
- Tubular sections can be formed without a side core.
| Part example | Key requirement met |
|---|---|
| Instrument or tool handle | Light weight with good stiffness |
| Small appliance housing with thick ribs | Reduced sink on the cosmetic surface |
| Bracket or frame with tubular section | Uniform wall without long hold time |
Key Takeaway: In practice, gas assist suits small and medium precision parts where a few thick features cause sink, warpage or long cycles.
Does gas assist injection molding reduce surface blemishes?
How can gas assist reduce sink-mark risk?
Gas-assisted molding can reduce sink risk by applying pressure through a designed gas channel as the outer skin cools. Results depend on channel continuity, gas timing and pressure, resin, wall transitions and the process window; use the sink-mark troubleshooting guide to structure diagnosis of the actual defect.
It gets better.
- Consistent pressure throughout the part.
- Localized shrinkage risk in thick ribs must be checked during mold trials.
- Appearance improvements must be checked against the approved surface standard.
| Blemish Type | Gas Assist Solution | |
|---|---|---|
| Sink Marks | Internal pressure packing | |
| Warping | Reduced internal molded-in stress | |
| Shadow Marks | Controlled gas channel placement |
Key Takeaway: Gas assist can reduce sink-mark risk over thick structural features, but the result must be confirmed during mold trials against the agreed appearance criteria.
Gas-flow control can support appearance goals, but flatness and defect acceptance must be measured on the actual geometry against the agreed standard.
How does gas assist injection molding impact tool longevity?
Why does low pressure benefit the mold?
The process operates at much lower pressures than conventional molding, which drastically reduces the mechanical wear and tear on your tooling. This means you can often utilize high-quality aluminum molds or lower-cost steel, extending the life of your investment.
Think about the possibilities.
- Less abrasive wear on the cavity.
- Reduced stress on the mold base.
- Lower maintenance costs over time.
| Metric | Gas Assist Impact | |
|---|---|---|
| Clamping Force | Can be lower for a validated design | |
| Tool Wear | Significantly lower erosion | |
| Maintenance Cycle | Longer intervals between servicing |
Key Takeaway: Protecting your tooling through low-pressure gas assist results in a lower total cost of ownership over the product’s lifecycle.
Molds subjected to lower stress maintain their precision for more cycles, ensuring consistent part quality for years to come.
Is gas assist injection molding better than thermoforming?
How does gas assist compare to vacuum forming?
Gas-assisted molding is often a better choice for medium to high volumes because it molds features like bosses and ribs directly into the part. While thermoforming requires expensive secondary CNC machining service for these features, gas assist delivers a finished part straight from the mold.
Keep this in mind.
- No secondary gluing or bonding.
- Higher dimensional repeatability.
- Better surface detail and texture.
| Feature | Gas Assist vs. Thermoforming | |
|---|---|---|
| Integrated Detail | Molded-in vs. Secondary Assembly | |
| Repeatability | High vs. Moderate | |
| Unit Cost | Lower at scale vs. Higher labor |
Key Takeaway: Compare gas assist and thermoforming using geometry, detail, tooling, volume, secondary operations and acceptance criteria; neither route is universally lower-cost or higher-quality.
The business case should include gas-control equipment, tooling, validation, labor, secondary operations and expected production volume.
How are gas pin and overflow locations approved?
Gas pin and overflow locations should be approved before the mold steel is cut, because they decide where the gas enters, how far it travels and where witness marks appear on the part.
What does the approval package include?
- Gas pin location on a thick section, away from cosmetic surfaces
- Gas channel path along the thick features
- Overflow cavity location and volume, if used
- Witness marks from pins and overflow gates marked on the drawing
- Flow simulation showing gas penetration
For example, on a handle the gas pin is usually placed near the gate end of the thick section, and an overflow well at the far end lets the gas push resin out to finish the hollow core. Our guide to parting line injection molding explains how witness marks are agreed on drawings. Test methods for checking molded plastic parts are published by ASTM International.
Key Takeaway: For this reason, agree gas pin, overflow and witness mark locations with the customer at the design review stage.
How is gas channel shutoff and leak tightness verified?
Gas channel shutoff and leak tightness are verified so that nitrogen enters only where it should and holds pressure until the part is packed.
Which checks are used?
- Pressure decay test of the gas circuit before trial
- Seal and O-ring inspection on gas pins
- Shutoff check between the gas channel and other mold areas
- Trial parts sectioned to confirm gas penetration
- Repeat checks during scheduled mold maintenance
For instance, a gas pin with a worn seal may leak pressure into the parting line, causing incomplete hollowing or blow-through. A short pressure hold test at each maintenance stop catches this early. Our plastic injection molding service includes these checks for gas-assisted parts.
Key Takeaway: Overall, a leak-tested gas circuit gives repeatable hollow sections from shot to shot.
Frequently Asked Questions
Does gas assist work with all types of plastic?Yes, most thermoplastic resins are compatible, though material selection is critical for gas channel performance.
Can gas assist make my parts lighter? It can reduce resin in suitable thick sections by forming a designed hollow channel. The actual weight change depends on geometry, channel development, strength requirements and the accepted process window.
Is the gas assist equipment very expensive?While it requires a gas controller, the savings in press tonnage and material often result in a net cost reduction.
Will I see holes in my part from the gas injection?Gas entry points are strategically placed in non-visible areas or within the runner system to maintain aesthetics.
Is gas-assisted molding good for small parts?Yes, when a small or medium part has thick handles, ribs or tubular sections that would otherwise sink or warp.
Optimize Your Production Today
Gas assist is a project-specific option for managing thick sections, mass, sink risk or part consolidation. WOKE Molds can review the geometry, resin, gas-channel concept and validation requirements; formal DFM normally follows project launch. Contact our team with the 3D model, drawing, volume, appearance criteria and target timing to discuss whether gas-assisted injection molds fit the project.