
ABS Injection Molding
ABS injection molding melts a selected acrylonitrile butadiene styrene grade and injects it into a purpose-built mold. ABS can offer a useful balance of impact behavior, surface finish and processability, but the result depends on the exact grade, additives, part geometry, tool and validated process window. Use an injection molding material selection guide to compare ABS with alternatives before freezing the specification.
What is the process of ABS injection molding?
The process feeds a selected ABS grade into a heated barrel and injects the melt into a machined cavity. Production volume and dimensional capability depend on the part, grade, tool, machine, process window and inspection plan.
Understanding Material Composition
ABS is a terpolymer whose formulation can balance chemical behavior, impact response, stiffness, flow and finish. The balance varies by grade and additives, so supplier data and molded-part testing govern selection.
- Acrylonitrile: Enhances heat resistance and chemical durability.
- Butadiene: Increases toughness and impact absorption.
- Styrene: Provides surface hardness and aesthetic shine.
Here is the kicker: the ratio of these components can be adjusted to meet specific engineering requirements for your unique application.
The Stages of the Molding Cycle
The injection cycle consists of four primary stages: clamping, injection, cooling, and ejection. Once the mold is closed, the screw moves forward to inject the melted ABS, followed by a holding phase to ensure the cavity is fully packed.
- Clamping: Secures the mold halves against high injection pressures.
- Injection: High-speed filling of the mold cavity with molten resin.
- Cooling: Solidification of the part to its final shape.
- Ejection: Mechanical removal of the finished part from the tool.
Cycle management can reduce residual-stress risk, but performance must be checked on conditioned molded parts under the intended load and environment.
Key Takeaway: A controlled molding cycle helps manage variation; physical properties and appearance still require project-specific process validation and inspection.
| Cycle Phase | Critical Control Point | User Benefit | |
|---|---|---|---|
| Injection | Speed and Pressure | Flash risk to verify during trials | |
| Cooling | Temperature Delta | Dimensional behavior to inspect | |
| Ejection | Pin Placement | Ejection marks to evaluate |
A thorough analysis of the injection cycle allows for the optimization of throughput without sacrificing the structural integrity of the ABS resin.
Why should you choose ABS for your technical parts?
Engineers select this material because it offers one of the best balances between mechanical performance and manufacturing cost. You will find that ABS injection molding provides the rigidity needed for structural housings while remaining easy to process.
Superior Mechanical Properties
Impact behavior and stiffness are reasons to evaluate ABS, but performance depends on the selected grade, part geometry, temperature, loading and test method. Review the supplier data and validate the part against its actual service requirements.
- Impact behavior: Verify the exact grade and molded part under the specified impact case.
- Tensile Strength: Review exact-grade mechanical data and validate the load-bearing geometry.
- Low Creep: Resistant to deformation over long periods.
You might be wondering if this durability comes at a higher price, but ABS remains remarkably affordable for mass production.
Excellent Finishing Capabilities
The molded surface can reproduce an approved polish or texture. Painting or electroplating, where specified, are separate finishing operations. Resin-grade suitability, surface preparation, adhesion and appearance must be qualified for the selected finishing process.
- Chrome Plating: A project-specific finish option whose adhesion and appearance require validation.
- Painting: Superior adhesion for custom branding.
- Texture: Hide wear and tear with molded-in grain.
Think about this for a second: the ability to finish parts easily reduces the need for secondary assembly steps.
Key Takeaway:Choosing ABS allows you to create parts that are as beautiful as they are strong, providing a professional finish that elevates your end product.
| Selection input | Evidence required | Part-level check | |
|---|---|---|---|
| Impact behavior | Exact grade, specimen conditioning, test method and temperature | Project drop or impact test | |
| Paint or adhesive bond | Grade, surface preparation and coating or adhesive specification | Adhesion and aging test | |
| Stiffness | Exact grade, conditioning, direction, temperature and test method | Assembly load and deformation check |
The synergy between surface energy and mechanical toughness makes ABS the most versatile choice for consumer-facing technical components.
How does ABS perform in high-heat environments?
ABS is an amorphous polymer that softens over a range rather than having one practical service-temperature limit. Glass-transition, HDT and other temperature values are grade- and test-condition-specific; none should be treated as a finished-part operating limit without the supplier data sheet and application testing.
Thermal Stability and Deflection
Heat deflection temperature (HDT) is a standardized test result measured under a stated load and specimen condition. Compare the exact ABS grade, test method, load and conditioning, then validate the molded geometry under its real temperature, load and exposure cycle.
- General-purpose ABS: Review the exact grade data rather than assuming a service-temperature ceiling.
- Heat-Resistant ABS: Engineered for higher thermal loads.
- Thermal expansion: Confirm the grade, orientation, geometry and temperature range used for design.
It gets even better when you realize that specialized additives can push these thermal limits even further.
Grade-Specific Thermal Limits
Flame-retardant or heat-modified ABS may be considered for an electrical housing, but the exact grade must be checked against the current supplier data and certification record. Flame classification depends on the test standard, specimen thickness, color and formulation; the finished assembly still needs its application-specific safety evaluation.
- Polylac PA-746: Balanced heat and flow properties.
- Flame-retardant grade: Verify the current rating, thickness, color and processing conditions for the named grade.
- Reinforced ABS: Filler level and orientation change stiffness, shrinkage, surface and tooling requirements.
Keep this in mind: selecting the wrong thermal grade can lead to premature part failure or melting in the field.
Key Takeaway: Select an exact grade from its current data sheet, then test the molded part under the project’s actual thermal, mechanical and environmental conditions.
| ABS option | Evidence to review | Application check | |
|---|---|---|---|
| General-purpose grade | Exact-grade mechanical and thermal data with test conditions | Actual load, temperature and exposure cycle | |
| Heat-modified grade | HDT, Vicat or other stated property without converting it to a service limit | Molded-part testing in the intended assembly | |
| Flame-retardant grade | Current classification, thickness, color and formulation | Applicable component and assembly requirements |
Consulting a technical data sheet helps you match the specific heat requirements of your application to the correct resin chemistry.
What are the primary design guidelines for ABS?
Part geometry is one important input for managing cost and defect risk during ABS injection molding. Use the material selection guide together with grade data, DFM and mold trials; no generic guideline ensures fill or release.
Wall Thickness Recommendations
Uniform walls are a useful design objective because abrupt mass changes can increase sink, warpage and residual-stress risk. Final wall thickness must come from the exact grade, structural needs, flow length, appearance zones, tool and trials.
- Uniformity: Reduces abrupt thermal and shrinkage transitions but does not remove warpage risk.
- Rib Ratios: Existing percentage ranges are starting points only; finalize them for the grade, load, surface and tool.
- Transitions: Use gradual fillets rather than sharp corners.
Let’s dig deeper into how wall design affects your bottom line by reducing the cooling cycle time.
Utilizing Proper Draft Angles
Draft supports mechanical ejection, but there is no universal minimum. Select it from depth, texture, exact grade, shrinkage, tool surface, ejection layout and acceptable marks, then confirm release during trials.
- Smooth-surface draft: Treat any handbook value as a starting point and review it for depth, grade, tool surface and ejection.
- Textured-surface draft: Obtain the texture supplier’s requirement and confirm it against depth and ejection direction.
- Internal Bosses: Require draft to prevent pin push marks.
Reviewing these features early can reduce avoidable tool-change risk, while T1 findings may still require modification.
Key Takeaway: Wall and draft guidance is a starting point; manufacturability and scrap risk must be evaluated for the exact part, grade, tool and process.
| Design feature | Selection input | Validation question | |
|---|---|---|---|
| Wall thickness | Grade, flow length, load, appearance and cooling | Do trials meet fill, sink, void and warpage criteria? | |
| Draft angle | Depth, texture, shrinkage, tool surface and ejection | Does the part release without unacceptable marks or distortion? | |
| Boss geometry | Fastener, load, wall intersection, coring and material | Do strength, sink and assembly tests meet requirements? |
Following these geometric constraints allows for a smoother flow of material and a more predictable shrinkage rate during the cooling phase.
Which industries rely on ABS molded components?
ABS is considered for housings, trim and other molded parts where its grade-specific balance of impact behavior, stiffness and finish fits the design. Automotive, electrical and medical projects add their own drawing, material, test, traceability and regulatory requirements.
Automotive and Transportation
Automotive projects may consider ABS for selected trim or housings, but each part requires its exact material specification, environmental tests, appearance criteria and applicable safety review.
- Interior Trim: High-quality aesthetic surface finish.
- Airbag-related components: Safety-critical geometry, material and deployment behavior require dedicated system-level validation.
- Instrument Panels: Structural rigidity and heat resistance.
Automotive programs require their own supplier scope, material specification, testing, documentation and part-approval evidence; ABS itself does not meet a quality-system standard.
Medical and Electronic Housings
Some ABS grades are marketed for selected medical-device or electrical applications. Verify the exact grade, colorants and additives, cleaning or sterilization exposure, electrical tests, intended contact type, market and current regulatory documentation before selection.
- Handheld Tools: Ergonomic and lightweight designs.
- Enclosures: High impact protection for PCB boards.
- Telephone Housings: Durable and resistant to skin oils.
Do not infer biocompatibility from the ABS family name. Any medical use requires the exact grade and formulation, intended contact and duration, relevant biological evaluation, processing controls and current project-specific documentation.
Key Takeaway:The wide adoption of ABS across diverse industries proves its reliability and fitness for both consumer-facing and industrial-grade applications.
| Industry | Typical Part | Material Priority | |
|---|---|---|---|
| Automotive | Door Handles | Mechanical strength | |
| Medical | Blood Pressure Monitors | Chemical resistance | |
| Electronics | Laptop Frames | Dimensional stability |
Industry examples are not acceptance standards. Select the grade and verification plan from the drawing, end-use environment, applicable market requirements and current supplier documentation.
How can you optimize mold designs for ABS?
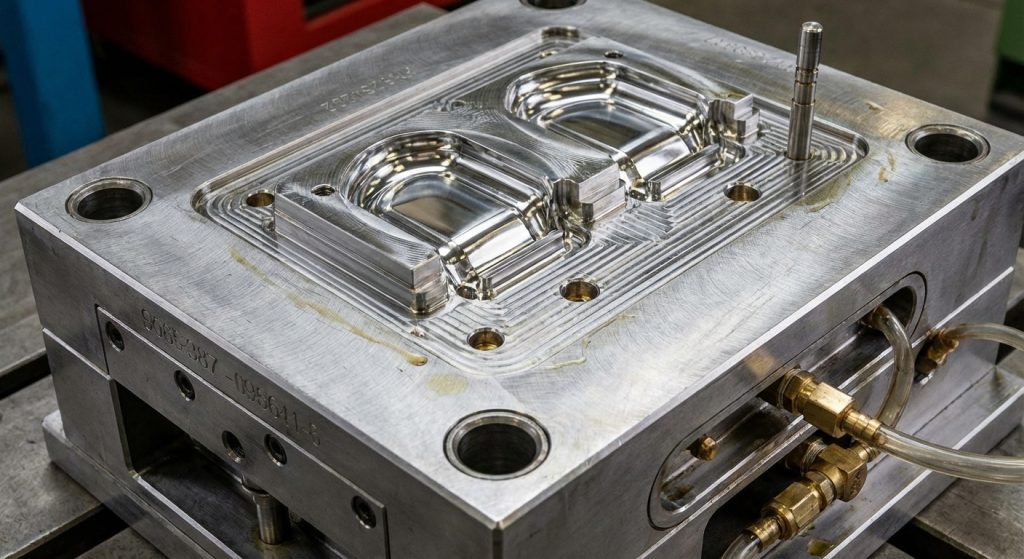
An ABS tool should account for the exact grade’s flow and shrinkage behavior. Gate and cooling decisions can reduce selected defect risks, but trials must confirm weld-line, appearance and dimensional results.
Strategic Gate Placement
The gate is where molten plastic enters the cavity, and its location influences filling and packing. A thicker region may be one candidate, but gate type and location must be evaluated for the exact grade, geometry, appearance zones and process rather than treated as a universal rule.
- Edge Gates: Simple and cost-effective for large parts.
- Sub-Gates: Automated degating for high-volume production.
- Hot Runners: Reduced waste and better pressure control.
Believe it or not, moving a gate just a few millimeters can sometimes solve a persistent quality issue.
Precision Cooling Channels
Effective cooling is the key to maintaining the dimensional accuracy of your custom molds . Because ABS is an amorphous polymer, it requires consistent cooling to prevent internal stresses that cause the part to warp after ejection.
- Conformal Cooling: Follows part geometry for even heat removal.
- Baffles and Bubblers: Cools deep bosses and core pins.
- Local inserts: Select insert material from thermal, corrosion, strength, wear and service requirements; stainless steel does not inherently mean faster heat transfer.
An optimized cooling layout may improve thermal balance or cycle stability, but the effect is project-specific and must be measured during controlled trials against the same part-quality requirements.
Key Takeaway: A well-engineered mold can reduce risk, while dimensional capability and tool life remain project-specific and must be verified against the drawing, resin, process and maintenance plan.
| Mold Feature | Optimization Goal | Production Impact | |
|---|---|---|---|
| Gate Location | Minimize Knit Lines | Structural strength | |
| Cooling Layout | Uniform Heat Removal | Less part warpage | |
| Surface Finish | SPI-A2 Polish | High-gloss aesthetics |
Using exact-grade flow data during tool design can identify risks before T1, while trial and inspection evidence are still required to close them.
What are the most common ABS resin grades?
Selecting the right grade of ABS is a critical step that dictates the final performance of your part. You must choose between standard, reinforced, or specialty grades based on the specific mechanical and environmental demands of your application.
Standard and Flame Retardant Grades
General-purpose and flame-retardant ABS grades are distinct formulations. For electrical work, review the current exact-grade record, test standard, specimen thickness, color and any processing restrictions; a material classification does not by itself approve the finished product.
- Standard Grade: Balanced impact and flow properties.
- Flame classification: Record the exact grade, standard, specimen thickness and color rather than treating a rating as a polymer-wide property.
- High-Flow Grade: For thin-walled or complex geometries.
Interestingly enough, the addition of flame retardants can slightly change the processing window, so your molder must be experienced with these resins.
Fiber Reinforced Variations
Glass-filled ABS grades can change stiffness, shrinkage, surface finish, anisotropy and tool wear. Use the exact manufacturer grade and reinforcement level, retain the stated test conditions, and validate the molded geometry rather than treating a filled grade as equivalent to neat ABS or metal.
- Glass-fiber level: Confirm the exact reinforcement percentage and orientation-sensitive properties from the grade data.
- Shrinkage behavior: Establish it for the exact grade, flow direction, geometry and process before setting tolerances.
- Higher HDT: Improved performance in warm environments.
Glass fibers can increase tool wear. Steel, hardness, coating, maintenance and spare strategy should be selected for the exact grade and project, without assuming a fixed mold life.
Key Takeaway: Matching the exact grade to the application helps manage cost and risk, but performance still requires molded-part validation.
| Grade category | Data to verify | Project trade-off | |
|---|---|---|---|
| General-purpose | Exact grade, flow, impact, stiffness, heat and finish data | Balance performance, processing and commercial needs | |
| High-flow | Test load and temperature, mechanical retention and shrinkage | Fill capability versus strength, appearance and warpage | |
| Reinforced | Filler level, direction, conditioning and exact test methods | Stiffness versus surface, anisotropy, wear and cost |
Selecting the ideal resin grade involves balancing the mechanical properties of the plastic with the processing capabilities of the injection equipment.
How do you solve quality issues in ABS molding?
ABS defects should be traced to material condition, geometry, tooling and process evidence. Documenting resin handling, trial settings and inspection results helps distinguish moisture, packing, cooling and ejection causes.
Eliminating Moisture Issues
ABS is hygroscopic, meaning it absorbs moisture from the surrounding air which can cause “silver streaks” or splay on the part surface. Proper drying is not optional; it is a requirement for high-quality ABS injection molding.
- Desiccant Drying: Removes internal moisture from resin pellets.
- Drying conditions: Follow the current exact-grade supplier data for temperature, time, dew point, initial moisture and material depth.
- Process Monitoring: Constant checks on the dew point of the air.
The bottom line is this: if you don’t dry your ABS resin, you will face structural weaknesses and cosmetic failures that are impossible to fix.
Managing Warpage and Shrink
Warpage occurs when different areas shrink differently, often because geometry, orientation, packing and cooling interact. Adjustments may reduce warpage, but flatness and dimensional acceptance must be demonstrated on inspected samples against the drawing.
- Cooling Time: Ensure the part is solid before ejection.
- Packing profile: May reduce sink when gate freeze, geometry and process allow; confirm during trials.
- Uniform Walls: The best defense against warpage.
CMM or other inspection methods can verify agreed features when the method, sampling plan, datum strategy and acceptance criteria are defined for the project.
Key Takeaway: Moisture control and thermal management are important inputs, but defect risk also depends on the exact grade, geometry, tooling, process window and inspection plan.
| Common Defect | Primary Cause | Proven Solution | |
|---|---|---|---|
| Silver Streaks | Excessive Moisture | Desiccant drying | |
| Sink Marks | Low Pack Pressure | Increase holding time | |
| Warpage | Uneven Cooling | Optimize water lines |
T1 evidence can identify likely causes and open actions; later trials and production monitoring must confirm whether each corrective action remains effective.
Is ABS molding suitable for rapid prototyping?
ABS may be useful for molded prototypes when the selected grade matches the intended evaluation. A 15–20 day figure should not be treated as an end-to-end promise: timing is project-dependent and must cover RFQ input review, engineering after launch, tool design and build, resin and component sourcing, T1, inspection, customer feedback, modification and any required T2/T3 before approval.
Functional Testing Accuracy
Molded prototypes can use the intended resin and process family, but they are not automatically identical to later production. Tool material, cavity layout, machine, process window and conditioning can change results, so each test must state what the sample represents.
- Real Materials: Test the actual resin used in production.
- Stress Testing: Validate mechanical limits accurately.
- Finish Testing: Confirm paint and plating adhesion.
This can expose selected design risks before production-tool investment, but prototype results do not remove the need for production-tool trials.
Bridge Tooling Benefits
Bridge tooling may suit a defined interim volume when its material, cavities, features, life, quality and change limits are agreed. Compare it with production tooling using project-specific cost, timing and validation needs.
- Project Schedule: Confirm engineering, tooling, sampling and approval milestones for the agreed scope.
- Lower Initial Cost: Reduced tooling investment.
- Scale Ready: Easily transition to mass production.
Generally speaking, ABS is one of the most cost-effective resins to use during this phase, making it a favorite for startups and hardware innovators.
Key Takeaway: ABS prototypes can support defined tests, but sample representativeness, validity and timing depend on the grade, tool, process and test plan.
| Method | Timing basis | What the sample can represent | |
|---|---|---|---|
| 3D printing | Project-dependent after file and process review | Selected geometry, fit or appearance checks | |
| Rapid tooling | Must include engineering, build, sourcing, trials and revisions | Defined resin and molding evaluations within the prototype-tool limits | |
| Production tooling | Project-dependent plan through required T1/T2/T3 and approval | Validation against the agreed drawing, resin and process plan |
Molded prototypes provide the most reliable path for verifying both the design and the material’s performance before capital commitment.
How to find the right ABS molding partner?
Review a prospective manufacturing partner’s engineering process, manufacturing scope, quality records and communication responsibilities. For ABS injection molding, agree how grade selection, tooling assumptions, trials and acceptance evidence will be handled.
Evaluating Quality Scope and Evidence
For automotive or medical sourcing, define the required quality system, supplier scope, part-specific controls and evidence before award. A certificate may be one procurement input, but it does not guarantee part performance or replace process, inspection and regulatory review.
- Automotive quality-system requirement: Verify the exact supplier scope and customer-specific requirements.
- Quality-system certificate: Check issuer, scope, site and validity; it does not certify an individual part.
- CMM Inspection: Verification of all critical dimensions.
Don’t forget that a certificate is only as good as the team behind it; always ask for sample inspection reports to verify their capabilities.
Global Engineering and Logistics
Agree the DFM timing, start point, inputs and deliverables for the project. Also define which party owns mold design, sourcing, molding, inspection, packaging, freight and import responsibilities rather than assuming one universal scope.
- DFM Support: Identifying cost-saving design changes early.
- Transparent Pricing: No hidden fees in your tooling quote.
- Logistics Support: Seamless export and customs handling.
Export experience can support communication and logistics planning, while responsibilities, documents, Incoterms and timing assumptions still need to be agreed for each order.
Key Takeaway: Evaluate a molding partner through relevant scope, technical review, trial evidence, inspection planning and transparent change control rather than a generic certification claim.
| Partner Attribute | User Value | Long-Term Impact | |
|---|---|---|---|
| Relevant quality scope | Documented project controls | Evidence-based supplier review | |
| Defined DFM scope | Review after project launch | Project-dependent development plan | |
| Export Expertise | Stress-free logistics | Reliable delivery |
The final decision on a molding partner should be based on their ability to demonstrate technical competence and consistent quality across multiple industries.
Conclusion
ABS injection molding decisions should connect the exact resin grade, part geometry, tool design, processing window and inspection plan. Compare ABS naturally with polycarbonate when clarity or impact behavior matters, and with polypropylene when low density, chemical resistance or living hinges matter. To review the drawing, resin requirement, volume and target timing, contact WOKE Molds.
Frequently Asked Questions
Can I target a high-gloss finish with ABS molding?Potentially. The exact grade, color, mold steel and polish, gate, venting and process affect gloss and defects; approve appearance against a defined texture or sample rather than assuming a mirror finish.
What is the best wall thickness for ABS parts?There is no universal best range. Use the exact grade, load, flow length, appearance zones, adjacent features, tool and process to select a starting geometry, then verify fill, sink, void, warpage and strength during analysis and trials.
How do I know if my design needs a modified ABS grade?Define the actual temperature, load, exposure cycle and applicable safety requirement, then compare exact grades using current supplier data. For flame behavior, retain the test standard, specimen thickness, color and formulation, and verify the finished application separately.
Can I use recycled ABS for injection molding?Potentially. Define the exact recycled grade or controlled regrind source, lot consistency, contamination limits, processing history, required properties and appearance, then validate molded samples. Do not assume a universal recycled-content threshold.
How long does a steel mold for ABS typically last?There is no universal cycle-life figure. Tool steel, hardness, construction, cavities, resin and fillers, surface requirements, maintenance, process and acceptance criteria all affect life; agree the project-specific mold-life and maintenance basis in the quotation.