
Practical Mold Cooling
Practical mold cooling applies thermal-management principles to support stable cycles and part quality in injection molding. Uneven mold temperatures can contribute to dimensional variation, warpage, and longer cooling phases. A sound cooling strategy considers channel layout, coolant conditions, and the molding material together rather than treating any one setting as a universal fix.
What defines effective and practical mold cooling?
Effective mold cooling is defined by the ability to remove heat at a rate that balances rapid cycle times with the structural integrity of the plastic part. You must look beyond simple chiller settings to analyze the actual energy transfer occurring within the tool steel. Practical mold cooling ensures that heat is extracted uniformly across the cavity to prevent localized stresses.
Achieving Thermal Balance
Think about it: If your cooling is uneven, your parts will warp as they shrink at different rates. You need to verify that your cooling channels are positioned to address the “hot spots” typically found in thick wall sections or near the gates.
Essential Cooling Metrics
- Gallons per minute (GPM) of flow.
- Pressure drop across the circuit.
- Temperature differential (Delta T) between inlet and outlet.
| Metric | How to Set the Target | What It Helps Assess | |
|---|---|---|---|
| Supply/return temperature difference | From the circuit heat load and process window | Heat removal and circuit balance | |
| Flow rate or Reynolds number | From channel geometry, coolant properties, and temperature | Flow regime and convective heat transfer |
Correct metrics allow you to maintain a steady-state condition where the heat added by the resin matches the heat removed by the water.
Key Takeaway: Measuring flow, supply and return temperatures, and cycle behavior provides evidence for diagnosing cooling variation across shifts.
Why is turbulent flow critical for mold cooling?
Turbulent flow can improve convective heat transfer by mixing fluid near the channel wall and reducing the insulating effect of a laminar boundary layer. The relevant Reynolds-number threshold depends on channel geometry, coolant properties, temperature, and surface condition, so flow targets should be evaluated circuit by circuit. For the wider production context, see this guide to estimating molding cycle time.
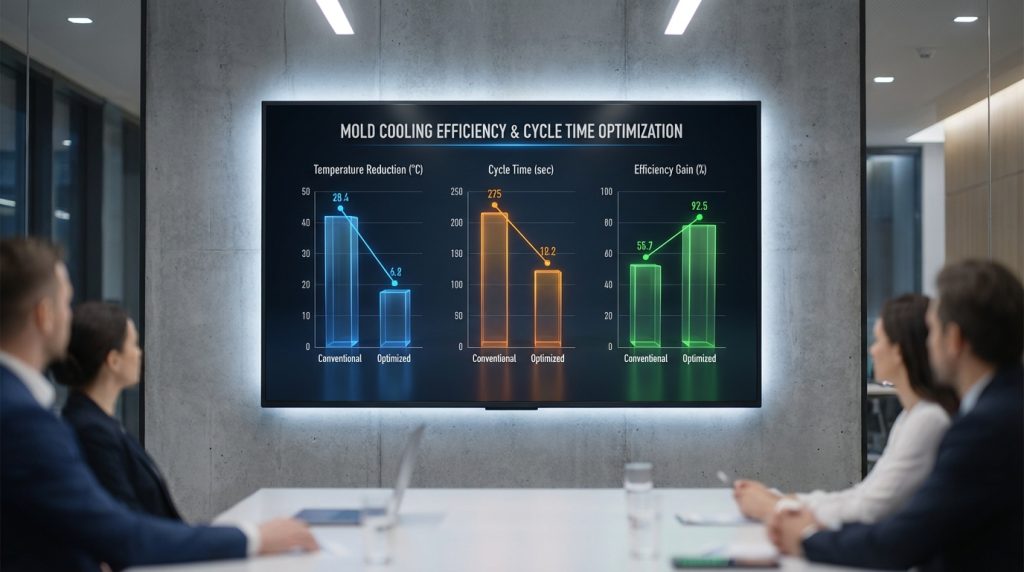
The Reynolds Number Factor
Here is the deal: You cannot simply increase pump pressure and hope for the best without understanding the fluid dynamics involved. The Reynolds number is a dimensionless value that helps you determine if your flow is laminar or turbulent based on velocity and viscosity.
- Low Reynolds Number: Laminar flow (Inefficient).
- High Reynolds Number: Turbulent flow (Efficient).
Flow Rate Requirements
| Input | Why It Matters | Verification | |
|---|---|---|---|
| Hydraulic diameter and channel condition | Define the flow area and resistance | Use the as-built circuit dimensions | |
| Coolant temperature and properties | Affect viscosity, density, and Reynolds number | Calculate at the operating condition |
Lower water temperatures require higher flow rates to achieve turbulence because the water is more viscous when cold.
Key Takeaway: Ensuring your system operates in the turbulent regime maximizes the thermal efficiency of every gallon of water pumped through your tool.
How does part thickness impact mold cooling cycles?
Part thickness impacts mold cooling by acting as a natural insulator that slows the rate at which heat can escape from the center of the plastic to the mold walls. Most unfilled resins transfer heat much slower than the tool steel, meaning the plastic itself often becomes the bottleneck in your production speed. Practical mold cooling for thick parts requires longer residence times rather than just colder water.
The Insulation Effect
But wait, there is more: The outer skin of a thick part solidifies quickly, creating a barrier that keeps the core temperature high for an extended period. If you eject the part too early, the internal heat will cause the part to warp or develop sink marks once it is out of the tool.
Critical Considerations for Thick Walls
- Use slower, steady cooling to prevent surface defects.
- Place cooling channels closer to thick ribs or bosses.
- Consider beryllium copper inserts for high-heat areas.
| Wall Condition | Cooling Consideration | Review Focus | |
|---|---|---|---|
| Thinner, uniform wall | Heat has a shorter path to the mold | Fill, pressure, and local hot spots | |
| Thicker or non-uniform wall | Core cooling can become limiting | Cooling time, sink, and warpage |
The relationship between thickness and cooling time is not linear; doubling the thickness can quadruple the required cooling time.
Key Takeaway: Designing your parts with uniform wall thickness is the most effective way to reduce cooling-related delays and ensure dimensional stability.
Can heat recovery systems optimize mold cooling?
Temperature-control units and monitored cooling circuits can regulate coolant conditions for mold zones that require different operating temperatures. Control strategy, flow stability, and energy use depend on the equipment and process; throttling alone does not make a mold self-regulating. These factors also interact with the overall molding cycle time.
Throttling for Temperature Control
It gets better: By monitoring the return water temperature, these systems ensure that the mold stays at a steady-state temperature without the need for external heaters in some cases. This maintains a consistent thermal profile throughout the production run, even if the plant’s water pressure fluctuates.
Benefits of Flow Regulation
- Reduced energy costs for cooling.
- Improved part surface finish (gloss).
- Consistent dimensions across long production runs.
| Feature | Impact on Production | Efficiency Gain | |
|---|---|---|---|
| Electronic Monitoring | Real-time adjustments | High | |
| Automated Valves | Constant Delta T | Medium |
Automation can reduce manual adjustment and make cooling conditions easier to monitor, although resin, machine, tool, and ambient variation still need process control.
Key Takeaway: Utilizing heat recovery and automated flow control allows you to maintain precise mold temperatures while lowering the total cost of operation.
What hardware components improve mold cooling performance?
High-performance hardware components like large-diameter hoses, high-flow manifolds, and specialized quick-connect fittings improve mold cooling by reducing the overall resistance to water flow. Many shops use undersized fittings that act as bottlenecks, preventing the system from ever reaching the velocity required for turbulent flow. Upgrading your hardware ensures that your pumps can deliver the full volume of water to the tool.
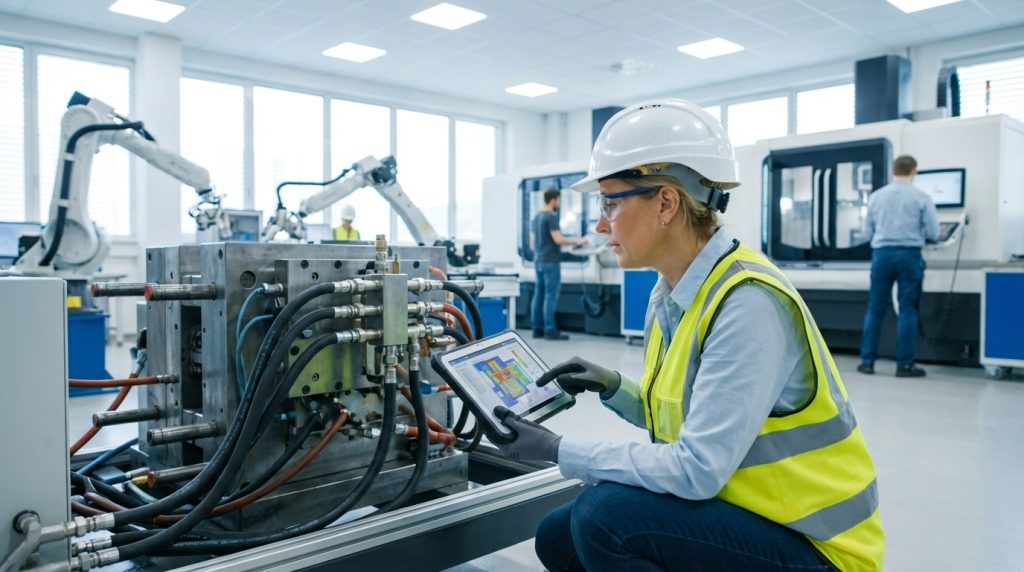
Eliminating Flow Obstructions
The bottom line is this: Every 90-degree elbow and narrow fitting in your circuit creates a pressure drop that steals energy from your cooling system. You should strive for the straightest paths possible and use full-port valves to maximize the volume of water reaching the internal channels.
Recommended Hardware Upgrades
- Use 300-series quick-connects over smaller 200-series.
- Switch to high-flow water manifolds with large inlets.
- Implement smooth-bore hoses to reduce friction.
| Component | Standard Choice | High-Performance Choice | |
|---|---|---|---|
| Fittings | 1/4″ NPT | 1/2″ NPT | |
| Manifold | Small Port | Large Plenum |
Higher-capacity hardware may reduce circuit restrictions when the pump, manifold, fittings, and channel geometry are sized as one system.
Key Takeaway: Optimizing the physical connections between your chiller and your mold is a simple, cost-effective way to immediately improve cooling efficiency.
Are manifold designs essential for mold cooling efficiency?
Manifolds distribute coolant among multiple mold circuits, but equal flow is not automatic. Circuit restriction, hose and fitting size, manifold geometry, and balancing all affect the flow each branch receives. Flow meters and a documented circuit layout can help verify the actual distribution as part of injection mold manufacturing and validation.
Balancing Flow Distribution
Make no mistake: The total area of the manifold inlet should be roughly equal to or greater than the sum of all the outlet areas. If the inlet is too small, the water velocity at the first few ports will be much higher than at the end of the manifold.
Manifold Best Practices
- Use stainless steel or aluminum to prevent corrosion.
- Color-code supply and return lines for easy setup.
- Install flow meters on every return line to verify flow.
| Manifold Feature | Purpose | User Benefit | |
|---|---|---|---|
| Large Plenum | Pressure stability | Uniform Cooling | |
| Integrated Meters | Visual verification | Rapid Troubleshooting |
Properly balanced manifolds eliminate the “chasing” of temperatures that often occurs when circuits are daisy-chained together.
Key Takeaway: Investing in well-engineered manifolds is the foundation of a professional and scalable cooling strategy for multi-cavity tools.
How do you calculate flow rates for mold cooling?
You calculate flow rates for mold cooling by determining the amount of heat energy (BTUs) that must be removed per hour and then solving for the required volume of water based on its heat capacity. This calculation ensures that your cooling system is physically capable of handling the thermal load of the specific resin and cycle time you are running. Accurate calculations prevent the installation of insufficient cooling that would otherwise lead to production delays.
Determining Thermal Load
The calculation should account for resin throughput, its thermal properties, processing temperatures, and the heat removed by the mold circuit. Required flow then depends on the selected supply/return temperature difference, coolant properties, pressure loss, and circuit geometry; the acceptable target comes from the project process window rather than a universal range.
Necessary Variables for Calculation
- Shot weight and cycle time.
- Material specific heat (e.g., PP vs. PC).
- Desired Delta T (Temperature change).
| Material | Heat to Remove (per lb) | Cooling Difficulty | |
|---|---|---|---|
| Polypropylene | High | High | |
| Polycarbonate | Medium | Medium |
Scientific calculations remove the guesswork from your cooling setup, allowing you to size your chillers and pumps correctly from the start.
Key Takeaway: Thermal calculations during mold design help size cooling circuits and identify assumptions that should be verified during sampling.
Why should you prioritize DFM for mold cooling?
Prioritizing Design for Manufacturability (DFM) for mold cooling allows channel placement and geometry to be reviewed before steel is cut. Early review can identify likely hot spots, channel-to-feature clearances, and manufacturing constraints while changes are still easier to consider. The scope of simulation and thermal analysis remains project-dependent; see our Engineering & DFM overview.
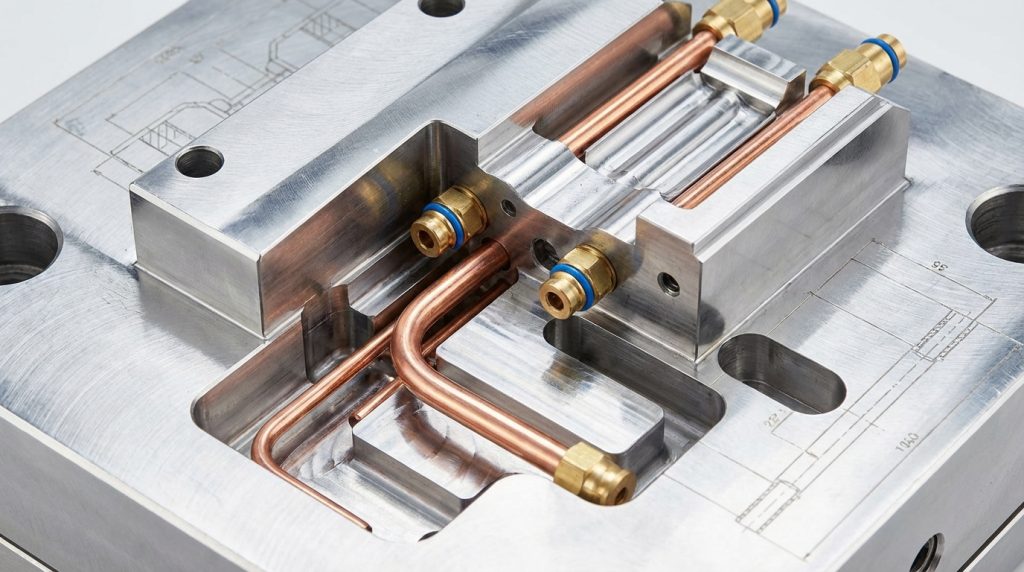
Proactive Thermal Management
Waiting until the first sample run to consider cooling can make changes more expensive. When appropriate for the project, thermal simulation can indicate likely temperature differences and help engineers evaluate baffles, bubblers, or revised channel layouts before sampling.
DFM Checklist for Cooling
- Confirm channel depth from the cavity surface.
- Check for clearance around ejector pins and lifters.
- Optimize the diameter of drilled passages for flow.
| DFM Step | Goal | Savings | |
|---|---|---|---|
| Simulation | Predict hot spots | Tooling rework costs | |
| Layout Review | Maximize coverage | Cycle time reduction |
A well-designed cooling layout supports stable processing and maintainability, but actual uptime also depends on the tool, machine, resin, water quality, and maintenance plan.
Key Takeaway: Effective cooling starts on the computer screen; a thorough DFM review is the best insurance policy against poor mold performance.
Can water chemistry affect your mold cooling system?
Water chemistry can affect a mold cooling system because mineral buildup or corrosion inside channels can restrict flow and add thermal resistance. The effect varies with deposit composition, thickness, channel geometry, and operating conditions. Monitoring and treating the circulating water helps protect molds and cooling hardware over time.
The Problem with Scale
But wait, there is more: Hard water contains minerals like calcium and magnesium that precipitate out of the water when it hits the hot surfaces inside the mold. This buildup not only blocks heat but also restricts flow, eventually leading to a complete blockage of small cooling circuits.
Water Quality Maintenance Tips
- Use a closed-loop system with treated distilled water.
- Regularly test pH and glycol levels to prevent corrosion.
- Implement filtration to remove particulates and biological growth.
| Issue | Cause | Effect | |
|---|---|---|---|
| Scaling | High Mineral Content | Blocked heat transfer | |
| Corrosion | Low pH / Oxidation | Internal channel damage |
Regular maintenance of your water system protects your high-precision tooling from irreversible damage and ensures consistent cooling performance.
Key Takeaway: Clean water is a prerequisite for efficient cooling; neglect your water chemistry, and your production efficiency will inevitably decline.
How do specialized materials enhance mold cooling?
Specialized materials and conformal cooling address different parts of the thermal problem. Copper-alloy inserts may offer higher material conductivity than common tool steels, while 3D-printed conformal inserts are primarily valuable because they can place coolant passages closer to complex cavity geometry. Their performance depends on alloy choice, channel design, flow, tool strength, and the application. See the conformal cooling design checks for project-specific considerations.
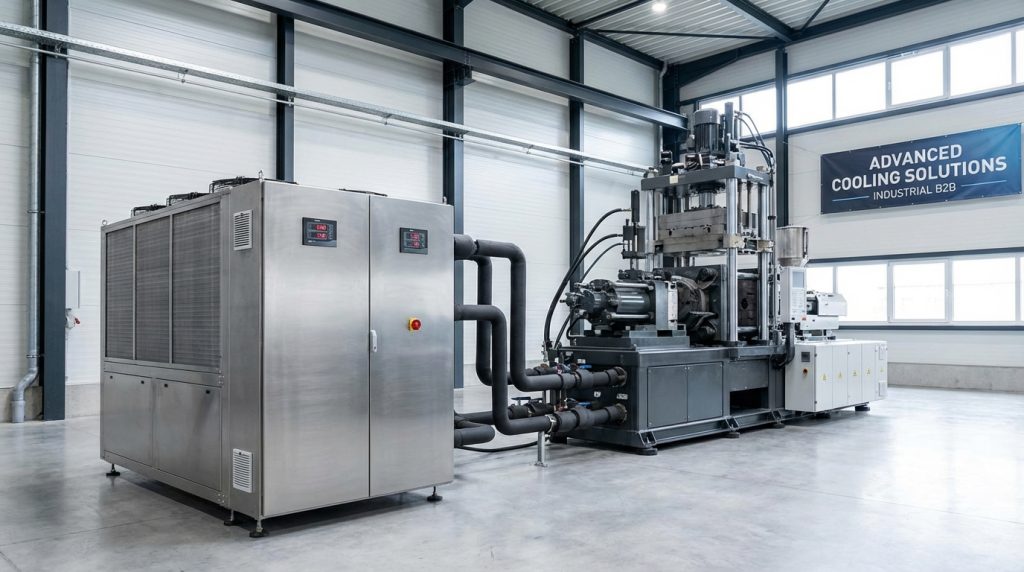
High-Conductivity Inserts
Copper alloys can conduct heat more readily than many tool steels, which may help move heat away from localized hot spots. Material selection must also account for strength, wear, corrosion, machining, safety, and compatibility with the mold design; it is not interchangeable with the geometric advantage of conformal water channels.
Advanced Cooling Techniques
- Beryllium copper cores and inserts.
- Conformal cooling channels via DMLS.
- Heat pipes for remote heat extraction.
| Material | Thermal Conductivity | Best Use Case | |
|---|---|---|---|
| Tool Steel | Low | Standard cavity/core | |
| Copper Alloy | High | High-heat cores/bosses |
Strategic use of materials allows you to solve the most difficult cooling challenges that traditional machining cannot address.
Key Takeaway: Material conductivity, water-channel geometry, and coolant flow are separate design levers that should be evaluated together for the specific mold.
Conclusion
Practical mold cooling connects channel design, coolant flow, tool materials, and process validation. Reviewing these factors during tooling development can reveal thermal risks before production decisions are finalized. To discuss the cooling requirements and evidence needed for your project, contact us.
FAQ
Can I use high-flow fittings on an old mold?Absolutely. Replacing restrictive small fittings with high-flow versions is one of the fastest ways to increase water velocity and potentially reach turbulent flow.
What is the best way to detect a blocked cooling channel?Compare circuit flow and pressure behavior with an established clean-condition baseline. A change can indicate restriction, but fittings, valves, pump performance, leaks, and measurement error should also be checked before concluding that a channel is blocked.
How do I know if my flow is turbulent?Calculate the Reynolds number. You need to know your water temperature, flow rate, and the diameter of your cooling channel to perform this calculation.
Can I run my mold without a chiller?It depends on the material and cycle time. While tower water is cheaper, it is often too warm to achieve the rapid cooling required for high-volume thermoplastic production.
How often should I clean my cooling channels?Set the interval from water-quality records, flow and pressure trends, tool documentation, material compatibility, and inspection findings. Use a cleaning method approved for the mold materials and cooling equipment rather than applying one fixed calendar interval.