
Thin Wall Injection Molding Tips and Considerations
What Defines Thin Wall Injection Molding Today?
Thin-wall injection molding describes parts whose wall section and flow-length-to-thickness ratio create a narrow filling window. The practical boundary depends on resin grade, geometry, gate location, machine response and the required part performance; thinner sections often need faster filling and careful pressure control.
How does the industry classify these dimensions?
The classification of these dimensions depends heavily on the specific resin and part complexity you are utilizing for the project. Let’s dive in:
- Thin-wall classification depends on resin, flow length, geometry and the required performance.
- Very thin features require project-specific fill, venting, cooling and ejection review.
- Critical tolerances must be defined on the drawing and validated for the selected material, geometry and process.
Key Takeaway: Understanding the threshold of thin-wall geometries helps you determine if your project requires high-speed machinery or specialized high-flow resins.
| Geometry Type | Typical Thickness | Pressure Requirement | |
|---|---|---|---|
| Standard | Project-specific baseline | Depends on resin and geometry | |
| Thin Wall | Narrower filling window | Evaluate fill and clamp demand | |
| Ultra-Thin | Very thin or long-flow features | Requires project validation |
The thickness of your part dictates the entire molding strategy and the choice of injection equipment.
Why Is Material Flow Critical in Thin Walls?
Material flow determines whether the molten resin can reach the furthest extremities of the cavity before the high surface-area-to-volume ratio causes it to solidify. In thin wall injection molding , the melt has significantly less time to travel, making flow length a primary constraint.
What happens when the melt freezes too early?
When the resin cools too rapidly, it creates a phenomenon known as “freeze-off” that prevents the cavity from filling completely. Think about it:
- Short shots occur at the furthest edges of the mold.
- Weak knit lines form where two flow fronts fail to fuse.
- Internal stresses increase as the machine forces material into narrow gaps.
Key Takeaway: Managing flow resistance through high injection speeds is essential to prevent structural defects in delicate plastic components.
| Flow Issue | Root Cause | Primary Symptom | |
|---|---|---|---|
| Freeze-off | Rapid cooling | Incomplete part | |
| Knit Lines | Low melt heat | Structural weakness | |
| Flash | Excessive pressure | Unwanted material |
Ensuring consistent flow protects your parts from the most common failure points in high-speed manufacturing.
Which Resins Suit High-Flow Requirements Best?
The best resins for thin wall injection molding are those with high melt flow indices (MFI) and low viscosity at high shear rates. Polypropylene (PP), High-Density Polyethylene (HDPE), and certain grades of Polyamide (Nylon) are the industry standards for these applications.
Why avoid high-viscosity materials like Polycarbonate?
High-viscosity materials like Polycarbonate resist flowing into tight spaces and require extreme temperatures that may degrade the polymer. Here is the kicker:
- Polypropylene flows easily into hinges and thin ribs.
- Nylon offers high strength even at reduced wall thicknesses.
- Liquid Silicone Rubber (LSR) fills complex geometries but risks flashing.
Key Takeaway: Selecting a high-flow resin reduces the pressure requirements on your mold and minimizes the risk of cosmetic defects.
| Material Type | Flow Rating | Strength Profile | |
|---|---|---|---|
| Polypropylene | Excellent | High Flexibility | |
| Nylon (PA) | Good | High Durability | |
| Polycarbonate | Poor | High Impact |
Resin choice is the foundation of a successful thin-wall project and directly impacts the longevity of your tooling.
How Does DFM Reduce Your Production Risks?
Design for Manufacturability (DFM) identifies potential molding bottlenecks during the digital CAD phase before you commit to expensive steel tooling. A formal engineering and DFM review can assess wall transitions, draft, gating, venting, cooling and ejection after project launch; simulation is used when project complexity or customer requirements justify it.
Can DFM prevent expensive mold modifications?
Identifying a “gas trap” or a “thin steel” condition in the design phase is significantly cheaper than modifying a hardened mold later. Let’s dive in:
- Draft analysis ensures parts eject without scratching.
- Gate location optimization prevents visible knit lines.
- Wall thickness checks pinpoint areas prone to short shots.
Key Takeaway: A formal DFM review can identify tooling and molding risks before steel decisions are finalized, but the commercial effect depends on the project.
| DFM Check | Purpose | Decision value | |
|---|---|---|---|
| Draft Analysis | Easy ejection | Prevents part scrap | |
| Flow Simulation | Predicts shorts | Prevents mold rework | |
| Gate Analysis | Surface finish | Reduces cosmetic scrap |
A thorough engineering review is the most effective way to ensure your project stays on schedule and within budget.
Should You Use Ribs for Structural Support?
You should use ribs to add structural stiffness to thin-walled parts because they provide strength without significantly increasing the overall mass or cooling time. In thin wall injection molding, ribs are essential for preventing the primary surfaces from bowing or collapsing.
What is the ideal rib-to-wall thickness ratio?
To avoid unsightly sink marks on the aesthetic surface of your part, the rib should be roughly half the thickness of the base wall. But wait, there’s more:
- Size ribs from the resin, wall section, load path and appearance requirements; validate the ratio for the actual part.
- Add gussets for cross-support in high-stress areas.
- Incorporate draft angles on rib walls for clean release.
Key Takeaway: Properly designed ribs provide the necessary rigidity for thin components while maintaining high aesthetic quality.
| Feature | Recommended Ratio | Primary Benefit | |
|---|---|---|---|
| Rib Thickness | 0.5x Base Wall | Prevents sink marks | |
| Rib Height | < 3x Base Wall | Prevents ejection issues | |
| Draft Angle | 1.0° – 1.5° | Smooth release |
Strategic ribbing allows you to maintain thin profiles while meeting the mechanical demands of your application.
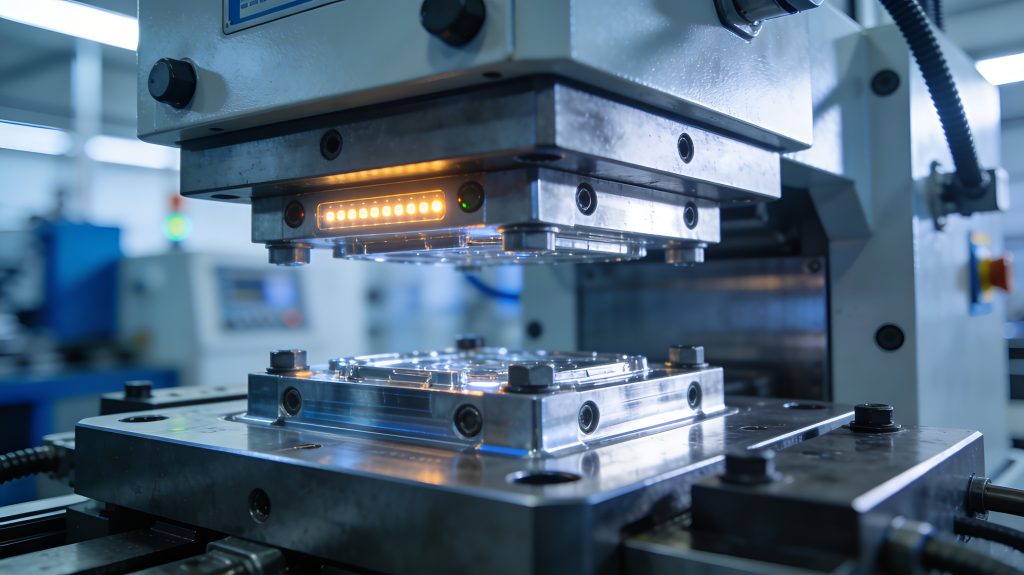
Why Does Uniform Thickness Prevent Part Warp?
More uniform wall thickness can reduce differential cooling and shrinkage, although resin, geometry, gate location and process settings still affect stress and warpage. In thin wall injection molding , even a slight variation in thickness can cause the part to twist as it contracts.
How does uneven cooling impact dimensions?
When one area of a part stays hot longer than another, the resulting differential shrinkage pulls the geometry out of alignment. The bottom line:
- Symmetrical designs cool more evenly.
- Gradual transitions prevent stress concentration points.
- Uniform walls allow for a more stable molding cycle.
Key Takeaway: Maintaining a constant wall thickness is the most effective design strategy for achieving dimensional stability in plastic parts.
| Cooling Factor | Impact | Solution | |
|---|---|---|---|
| Sharp Steps | High Stress | Use gradual tapers | |
| Thicker Bosses | High Sink | Core out heavy areas | |
| Large Flats | High Warp | Add reinforcing ribs |
Consistency in wall thickness is the hallmark of a professional plastic design optimized for high-volume production.
Can Radii Solve Ejection and Flow Issues?
Adding radii to internal and external corners improves material flow and reduces the force required to eject the part from the mold. In thin wall injection molding, sharp corners act as flow barriers and stress concentrators that can cause cracks.
Do rounded corners improve the part’s lifespan?
Rounded corners distribute mechanical loads across a larger area, preventing the part from failing under impact or stress. Think about it:
- Internal radii help the melt flow smoothly around turns.
- External radii prevent sharp edges from snagging.
- Radii reduce the risk of part deformation during ejection.
Key Takeaway: Incorporating radii throughout your design facilitates a laminar flow path and enhances the overall durability of the component.
| Feature | Min. Radius | Primary Function | |
|---|---|---|---|
| Internal Corner | 0.5x Wall | Flow optimization | |
| External Corner | 1.5x Wall | Stress reduction | |
| Ejection Path | Variable | Damage prevention |
Small geometric adjustments like adding radii make a significant difference in the manufacturability of complex thin-walled housings.
How Do You Manage Tight Molding Tolerances?
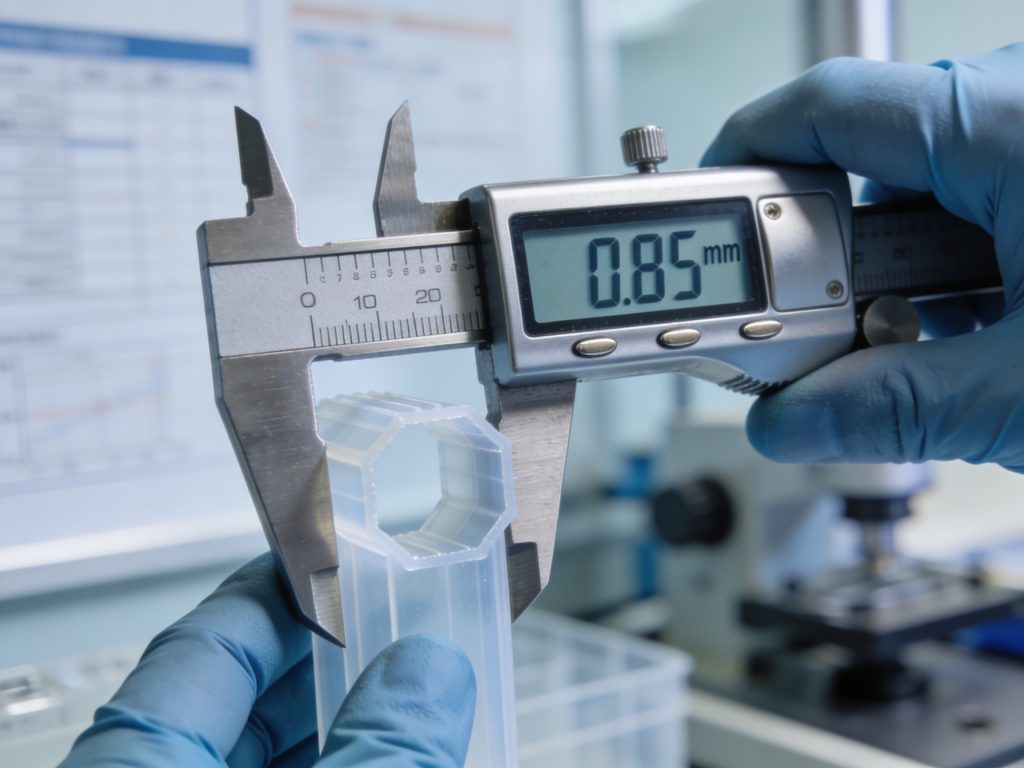
Managing tight tolerances in thin wall injection molding requires suitable equipment, a defined measurement method and process monitoring tied to the drawing CTQs. Inspection conditions and sampling should be agreed for the project.
Why is CMM inspection vital for these parts?
Coordinate Measuring Machines (CMM) provide the micron-level accuracy needed to verify that thin-walled features meet your engineering prints. Here is the kicker:
- Automated monitoring detects process drift early.
- Precision fixtures ensure consistent part orientation.
- Statistical process control (SPC) tracks quality trends.
Key Takeaway: Success in precision molding depends on the ability to measure and control every variable in the production environment.
| Control Tool | Measurement | Quality Benefit | |
|---|---|---|---|
| CMM | Defined dimensions | Drawing-based verification | |
| Pressure Sensor | Fill Repeatability | Consistent weight | |
| ERP System | Batch Tracking | Full traceability |
Inspection equipment can verify defined dimensions, but functional acceptance must follow the drawing, measurement plan and assembly requirements.
Is 2K Molding Effective for Thin Components?
Two-shot (2K) molding is highly effective for thin components because it allows you to integrate soft-touch grips or seals without secondary assembly. This process is frequently used in thin wall injection molding for consumer electronics and medical devices.
How does overmolding strengthen thin substrates?
Adding a second layer of material can provide structural reinforcement to a delicate thin-walled base part. Let’s dive in:
- Chemical bonding creates a permanent material connection.
- Integrated seals may reduce separate O-rings when the sealing design is validated.
- Multi-material parts can combine tactile, sealing or appearance functions.
Key Takeaway: 2K molding reduces your total assembly costs while providing functional benefits that single-material parts cannot achieve.
| Process Type | Materials | Key Advantage | |
|---|---|---|---|
| 2K Molding | Rigid + Soft | Integrated seal/grip | |
| Insert Molding | Metal + Plastic | Threaded strength | |
| Overmolding | Plastic + LSR | Enhanced protection |
Multi-material strategies are the future of complex part design, offering a level of integration that simplifies your supply chain.
How Should You Qualify a Thin-Wall Manufacturing Partner?
Qualify a thin-wall manufacturing partner against the project drawing, process-control plan, inspection method, traceability needs and any customer-specified quality-system requirements. Do not infer capability from a certification label alone; request the documents that apply to your program.
What evidence should you review for the project?
Ask how the supplier controls the narrow process window, records critical settings and verifies drawing requirements. Relevant evidence may include:
- Material traceability protects your supply chain.
- Corrective-action records show how recurring issues are contained and reviewed.
- Applicable audit and quality-system records can be reviewed when required by the customer.
Key Takeaway: Supplier qualification should connect documented controls and inspection evidence to the actual thin-wall part requirements.
| Evidence | Review focus | Project use | |
|---|---|---|---|
| Process-control plan | Critical settings and reactions | Part-specific control | |
| Inspection plan | CTQs and measurement method | Acceptance evidence | |
| Traceability records | Material, lot and revision | Customer-defined tracking |
Choosing a partner with the right credentials provides the peace of mind needed when launching critical new products.
Material selection, rib and wall design, gating, venting, cooling and inspection should be reviewed as one thin-wall molding system. WOKE Molds can discuss the project inputs and manufacturing route, with formal DFM normally beginning after project launch. Please contact our team and share the 3D model, 2D drawing, resin, critical dimensions, expected volume and target timing.
Frequently Asked Questions
Can I use any resin for thin-walled parts?No, you must select resins with a high Melt Flow Index (MFI) to ensure the material can fill thin cavities before it cools and solidifies.
What is the best way to prevent part warping?The best way is to maintain a uniform wall thickness throughout your design to ensure even cooling and minimize internal stresses during contraction.
How do I know if my design is too thin to mold? Review the wall section together with flow length, resin grade, gate location, venting, machine capability and the required CTQs. No single thickness threshold determines manufacturability.
Can I combine two materials in one thin part?Yes, 2K or double injection molding allows you to combine rigid and soft materials, which is excellent for adding grips or seals to thin components.
How long does it take to build a thin-wall mold? Timing depends on mold architecture, steel and component availability, validation scope, revisions and the agreed trial plan. Confirm a project schedule only after the design and acceptance requirements are reviewed.