
Original Equipment Manufacturer - OEM Plastic parts Supplier
An OEM plastic parts supplier produces custom components to a buyer’s drawing, material specification and acceptance criteria. Supplier evaluation should therefore focus on engineering review, tooling and molding resources, inspection planning, change control and evidence from comparable project requirements. WOKE Molds builds molds in our own factory in Dongguan and produces parts in our molding plant in Shenzhen.
What defines high-quality OEM plastic parts today?
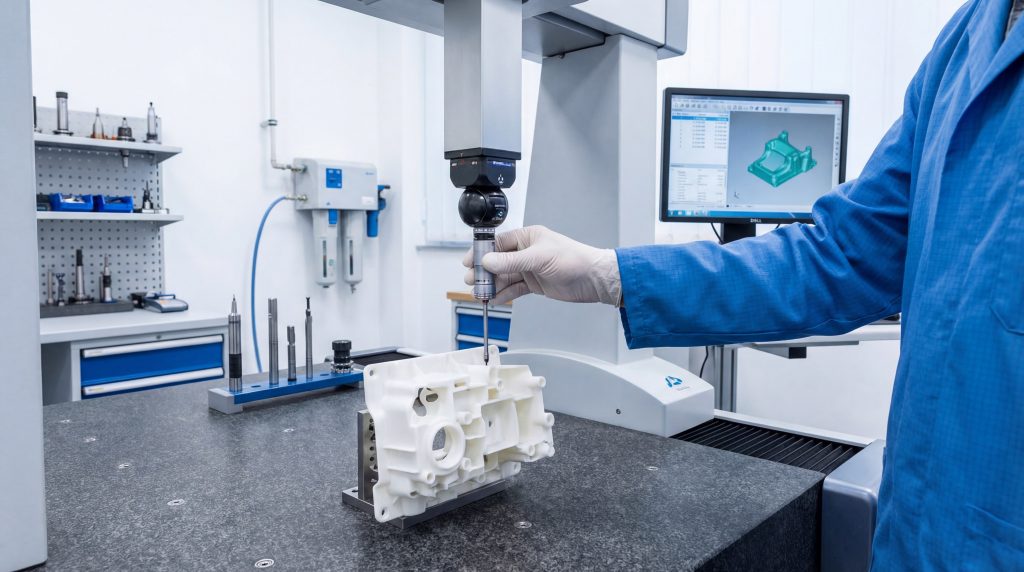
High-quality parts are defined by conformance to agreed drawings, material requirements, appearance standards and functional tests. For production sourcing, establish critical characteristics, sampling or inspection frequency, traceability and the response plan for nonconformance rather than assuming every unit is identical to a prototype.
Essential quality benchmarks
Modern manufacturing requires a combination of advanced machinery and rigorous inspection protocols to succeed. You must look for suppliers whose press range, such as 30–380 T for small and medium parts, matches varying part complexities.
Here is the deal:
- Dimensional tolerances defined by the drawing and verified with a suitable measurement method.
- Surface acceptance limits agreed for functional and appearance zones.
- Full material traceability for every batch.
Key Takeaway: Prioritizing precision and traceability ensures your components function reliably in critical assemblies.
| Quality input | Buyer should define | Project evidence | |
|---|---|---|---|
| Dimensions | Drawing, datum scheme and CTQs | Agreed dimensional or CMM report | |
| Appearance | Zones, limit samples and defect criteria | Visual inspection under agreed conditions | |
| Material | Exact grade, color and compliance needs | Supplier records or certificate when required |
The data above highlights how superior measurement technology directly translates to lower failure rates in your supply chain.
Why source OEM plastic parts from Guangdong?
Sourcing OEM plastic parts from Guangdong, including Dongguan and Shenzhen, can provide access to a concentrated network of mold, molding, machining, component and logistics resources. The commercial result depends on the actual tool specification, resin, validation scope, order volume, Incoterm and freight plan, so compare itemized quotations rather than relying on a universal regional saving.
Regional logistical advantages
Proximity to major ports can support global export, but transit time depends on destination, mode, routing, customs and the agreed Incoterm. Request a project schedule that separates tooling, trials, approval, production and freight instead of treating shipping as a fixed promise.
Believe it or not:
- Access to high-grade engineering resins.
- Rapid prototyping and CNC services nearby.
- Integrated supply chains for electronics.
Key Takeaway: Above all, the Guangdong manufacturing hub combines cost efficiency and technical depth, as our guide to injection molding in China explains.
| Quote factor | What changes it | What to compare | |
|---|---|---|---|
| Tooling scope | Steel, cavities, hot runner, finish and validation | Included build and trial scope | |
| Lead time | Complexity, materials and approval cycles | Milestones and assumptions | |
| Logistics | Destination, mode and Incoterm | Freight boundary and handoff |
This comparison clarifies why the Asian manufacturing corridor remains the preferred choice for high-volume production projects.
How does DFM affect your OEM plastic parts?
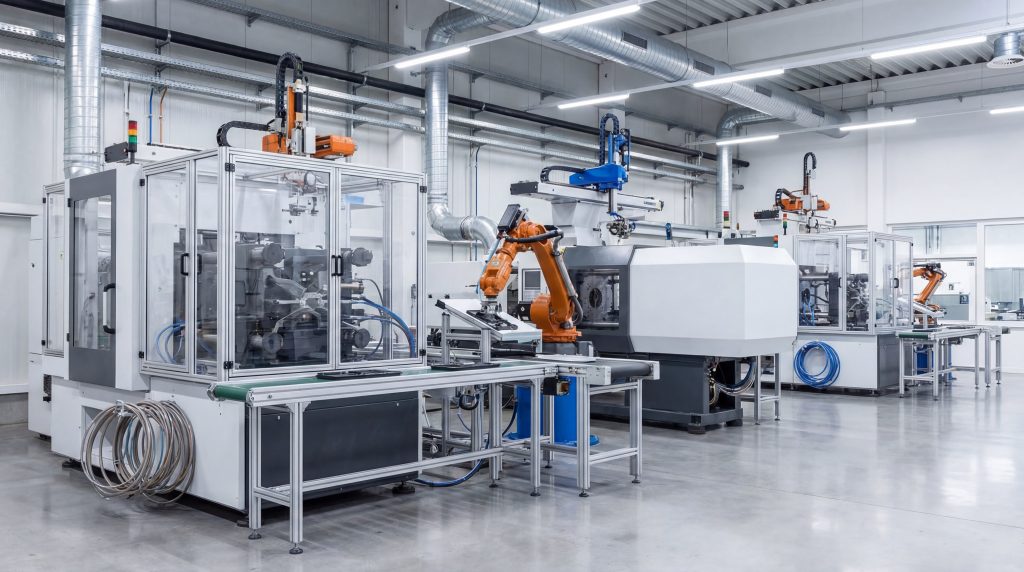
Design for Manufacturing (DFM) is the process of optimizing part geometry to ensure it can be produced efficiently and cost-effectively. Implementing a DFM review early in the development cycle helps you identify potential molding issues before they become expensive failures.
Impact on production speed
Optimized designs lead to shorter cycle times, which directly reduces your unit price over long production runs. You will see significant savings by adjusting wall thickness and gate placements to facilitate faster cooling.
The truth is:
- Uniform walls prevent part warping.
- Proper draft angles allow easy ejection.
- Rib designs add strength without weight.
Key Takeaway: Professional DFM optimization acts as a preventative measure that secures both part quality and project profitability.
| Design feature | Review question | Required evidence | |
|---|---|---|---|
| Wall thickness | Are heavy transitions creating cooling or sink risk? | Section review and trial result | |
| Draft angles | Can the part release without damage? | Tool design review and trial observation | |
| Gate location | Does filling affect weld lines, packing or appearance? | Engineering review and approved samples |
Strategic design choices early in the process result in cumulative savings that enhance your overall manufacturing margin.
How should a supplier’s quality system be evaluated?
Ask the supplier which quality-system requirements apply to the quoted manufacturing site and request current, scope-matched evidence when a certification is mandatory. Certification alone does not approve a part; the project still needs drawing review, material control, process records, inspection and an agreed response to nonconformance.
Risk management in production
For supply continuity, review contingency planning, critical subcontractors, material sources, tool maintenance and change notification as project inputs. Record responsibilities and escalation contacts rather than inferring resilience from a logo or certificate name.
Consider this:
- Reduced variation in part batches.
- Formalized root cause analysis for errors.
- Strict control over sub-tier vendors.
Key Takeaway: Verify site-specific quality evidence and connect it to the part’s inspection, traceability and change-control plan.
| Evidence | Buyer check | Project connection | |
|---|---|---|---|
| Certificate | Issuing body, site, scope and validity | Does the quoted site and process fall within scope? | |
| Control plan | Characteristics, method and frequency | Does it cover the drawing CTQs? | |
| Corrective action | Containment, cause, action and verification | How will escapes be closed? |
A quality-system certificate is one supplier-evaluation input, not a guarantee of a particular part outcome.
Which resins work best for OEM plastic parts?
The best resin depends on your part’s mechanical requirements, environmental exposure, and budget constraints. Engineering-grade plastics like Nylon (PA), ABS, and Polycarbonate (PC) are the most common choices for technical components.
Matching materials to performance
You must select a polymer that balances strength with manufacturability to avoid production bottlenecks. For example, Nylon provides excellent heat resistance, while ABS offers superior impact strength for consumer electronics.
But wait, there is more:
- PP is ideal for chemical resistance.
- PC/ABS blends offer high-end finishes.
- PEEK is reserved for extreme environments.
Key Takeaway: Correct material selection is the foundation of a part’s longevity and its ability to withstand operational stress.
| Resin Type | Key Property | Typical Use | |
|---|---|---|---|
| ABS | Impact Resistance | Housing/Cases | |
| Nylon (PA) | Heat Stability | Automotive Parts | |
| Polypropylene | Chemical Proof | Medical Caps |
Understanding the chemical profile of these resins allows you to tailor your product for specific industry challenges and environments.
How to scale production for OEM plastic parts?
Scaling requires a transition from prototyping or low-volume runs to automated, high-tonnage production lines. You can effectively scale OEM plastic parts by investing in multi-cavity tooling that produces several units per cycle.
Automation and cycle efficiency
Automation and extended production schedules can support higher demand when the selected manufacturing resource, tooling, staffing and material supply are qualified for the project. Capacity and lead time should be confirmed from a calculation based on the actual cycle, cavities, uptime assumptions and release schedule.
The best part:
- Multi-cavity molds lower unit costs.
- Automated sorting reduces labor errors.
- In-process monitoring ensures stability.
Key Takeaway: Scalability is achieved through a combination of robust tooling design and high-capacity machine availability.
| Scale input | Tooling question | Evidence to request | |
|---|---|---|---|
| Annual demand | What cavity count and tool construction fit the forecast? | Capacity calculation with cycle and uptime assumptions | |
| Release pattern | How will batch size affect setup and inventory? | Production and delivery schedule | |
| Approval risk | Should the project validate before adding automation? | Trial, inspection and ramp plan |
Transitioning to multi-cavity tools is the most efficient method for driving down costs as your market demand grows.
Are thin-wall designs good for OEM plastic parts?
Thin-wall designs can reduce material usage and part weight, but they also narrow the filling and processing window. Wall thickness must be evaluated against flow length, resin grade, gate design, machine capability, stiffness, appearance and dimensional requirements; no universal material-cost saving applies.
Technical design considerations
Successful thin-walling requires specialized resins with high flow rates to ensure the cavity fills completely. You must also include strategic ribbing to maintain structural integrity in OEM plastic parts that are exceptionally light.
Keep this in mind:
- High-speed injection is mandatory.
- Conformal cooling improves cycle time.
- Venting prevents air traps and burns.
Key Takeaway: Thin-wall molding is a sophisticated technique that offers significant cost and weight advantages for modern product design.
| Design Factor | Thin Wall | Standard Wall | |
|---|---|---|---|
| Thickness | < 1.0mm | 2.5mm – 3.0mm | |
| Cooling Time | Extremely Fast | Moderate | |
| Pressure | High | Standard |
Designing for thin walls requires expert engineering to balance the benefits of lightness with the risks of part fragility.
What is the MOQ for custom OEM plastic parts?
There is no fixed general MOQ for custom OEM plastic parts at WOKE Molds. Order quantity is evaluated by project because tooling, setup, resin procurement, packaging, inspection and forecast requirements affect the commercial structure.
Flexibility for growth
For an initial batch, discuss forecast, tooling ownership, resin purchase constraints, setup charges and the approval plan. The quoted batch should align with validation needs and inventory risk.
Here is the secret:
- Higher volumes lower the unit price.
- Tooling costs are a one-time fee.
- Material waste is minimized at scale.
Key Takeaway: Treat order quantity as a project input and make setup, material and inventory assumptions visible in the quote; our guide to contract injection molding lists the terms to agree.
| Quantity input | Commercial effect | Buyer evidence | |
|---|---|---|---|
| Initial validation batch | Setup and inspection scope may dominate | Approval quantity and test plan | |
| Forecast production | Supports cavity and automation decisions | Annual demand and release pattern | |
| Resin purchase lot | Can affect minimum buy and inventory | Exact grade, color and shelf-life needs |
Finding the right volume threshold allows you to maximize your purchasing power while maintaining a lean inventory strategy.
Does 2K molding benefit your OEM plastic parts?
2K or two-shot molding allows you to combine two different materials or colors in a single manufacturing cycle. This process benefits your components by eliminating the need for secondary assembly and creating a superior chemical bond between materials.
Enhancing part functionality
You can use this technique to add soft-touch grips to rigid housings or create waterproof seals within a single part. It is particularly effective for high-end automotive interiors and medical devices.
Look at the facts:
- Reduces total assembly labor costs.
- Improves ergonomic feel and grip.
- Creates permanent material bonds.
Key Takeaway: Multi-material molding is a premium manufacturing solution that adds functional value and aesthetic appeal to your products.
| Process | Steps Required | Cost Impact | |
|---|---|---|---|
| 1-Shot + Assembly | 2 Cycles + Labor | Higher OPEX | |
| 2K Molding | 1 Cycle | Lower OPEX | |
| Overmolding | 2 Cycles | Moderate |
Utilizing advanced molding techniques like 2K simplifies your supply chain by reducing the number of individual parts you need to manage.
Why trust us for your next OEM plastic parts?
Evaluate WOKE Molds on the proposed engineering route, trial plan, inspection scope and project records. We build the molds in our Dongguan factory and run molding and machining in-house, but your technical requirements should be converted into drawing CTQs and agreed acceptance evidence before approval.
Engineering-first approach
Support can cover project review, mold development, trials, inspection coordination and logistics according to the quotation. Formal DFM normally follows project launch, and finished-part tolerances are evaluated per drawing, resin, geometry, tooling and measurement method rather than promised as one universal number.
The bottom line:
- Transparent communication throughout.
- DFM findings tied to part geometry and project requirements.
- Press range matched to small and medium precision parts.
Key Takeaway: Select the supplier whose quoted resources, controls and evidence match the part and production plan.
| Capability | Verified scope | Buyer check | |
|---|---|---|---|
| Engineering | Post-launch DFM; Moldflow when project needs justify it | Required review outputs | |
| Molding network | 30-380T class resources, including two-shot and micro-molding | Machine and process fit for the part | |
| Inspection | Key dimensions, CMM and reports can be arranged as required | Method, frequency and report format |
For regulated or safety-related projects, state the applicable customer, site, documentation and validation requirements in the RFQ and verify them before award.
Conclusion
Reliable OEM sourcing starts with complete inputs and a reviewable evidence chain. WOKE Molds can assess the 3D model and 2D drawing, then align resin, mold, molding, inspection and manufacturing inputs around the project. Include quantity, critical tolerances, appearance, documentation, target timing and logistics assumptions in your injection molding RFQ. Contact us for a project quotation; formal DFM normally follows project launch.
FAQ: Frequently Asked Questions
- Can I request a DFM review for my project?Start the RFQ with a 3D model and 2D drawing. Formal DFM and technical review normally follow project launch; the exact scope is agreed for the project.
- What is the best material for high-heat automotive parts?There is no universal best material. Select the exact grade against continuous and peak temperature, load, chemicals, moisture, flammability, dimensional stability and compliance requirements.
- How do I know if my part is suitable for thin-wall molding?Evaluate wall thickness, flow length, resin grade, gate design, machine capability, stiffness, appearance and dimensional requirements together.
- Can you support both prototypes and production?WOKE Molds can coordinate prototype, small-, medium- and mass-production requirements through the appropriate machining and molding resources. The quoted route depends on geometry, material, volume and validation needs.
- How are critical tolerances verified?Tolerances are reviewed per drawing and project. The inspection plan can include key dimensions, CMM or other suitable methods, with report scope and sampling agreed according to customer requirements.
For production support, explore our plastic injection molding service. You can also share your drawing for an engineering review.