
Clamping Force Calculation with a Worked Example
Clamping force calculation estimates how much force an injection molding machine must apply to keep the mold closed while plastic is injected. The basic formula multiplies the projected area of the parts and runner by the cavity pressure and adds a safety margin. The result decides the press size, which affects part cost, flash risk and whether a mold fits the plant.
A rough estimate is quick but needs judgment. For example, a thin-walled PC housing needs far more pressure per square centimeter than a thick PP lid of the same size, so using one pressure value for both would undersize the press for the housing. In this guide, we explain clamping force calculation: the formula, projected area, cavity pressure by resin and wall, a worked example, safety factors, press checks and when to use simulation. For press-side checks, see our guide to injection molding tool design.
Clamping force calculation uses F = A × P × S, where A is the total projected area of all cavities and runners in the opening direction, P is the average cavity pressure, and S is a safety factor of about 1.1–1.2. In metric units, force in kN = area in cm² × pressure in MPa ÷ 10. Average cavity pressure for estimates ranges from about 20–35 MPa for easy-flow resins and thick walls to 50–80 MPa for thin walls, long flow and high-viscosity or filled resins. The result is compared with press tonnage, tie-bar spacing, shot size and mold height before a machine is chosen.
In short: projected area × cavity pressure × safety factor gives the clamp force; then check the rest of the press. To run the numbers for your part, use our injection molding tonnage calculator.
Key points:
- Formula: F = A × P × S.
- Inputs: projected area, resin, wall thickness, flow length.
- Check: tonnage, tie bars, shot size, mold height.
What Is the Clamping Force Calculation Formula?
The clamping force calculation formula multiplies projected area by cavity pressure and a safety factor.
| Unit system | Formula |
|---|---|
| Metric | F (kN) = A (cm²) × P (MPa) ÷ 10 × S |
| Metric tonnes | F (t) ≈ F (kN) ÷ 9.81 |
| Imperial | F (US tons) = A (in²) × P (tons/in²) × S |
For example, 100 cm² × 40 MPa ÷ 10 = 400 kN, or about 41 tonnes before safety factor. Machine data and definitions for injection molding machines are covered by EUROMAP recommendations.
Key Takeaway: Above all, keep units consistent; most errors come from mixing them.
How Do You Measure Projected Area?
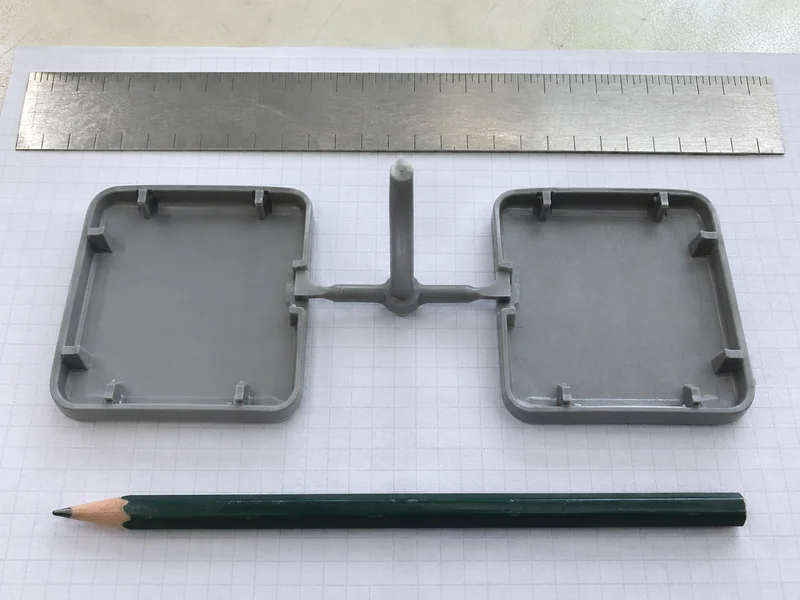
Projected area is the area of the parts and runner seen from the mold opening direction.
- Project each part onto the parting plane
- Include the runner and sprue footprint
- Multiply by cavity count
- Ignore holes that are fully closed off by shutoffs
- Include side-action areas only if they load the parting line
For example, a 60 × 40 mm lid has 24 cm² projected area; four cavities and a 6 cm² runner give 102 cm². Our guide to multi cavity injection molding shows how cavity count changes area.
Key Takeaway: In other words, projected area is a footprint, not the surface area of the part.
Which Cavity Pressure Suits a Clamping Force Calculation?
Cavity pressure depends on resin flow, wall thickness and flow length.
| Case (rule of thumb) | Average cavity pressure |
|---|---|
| Easy-flow resins (PP, PE), thick walls | about 20–35 MPa |
| General resins (ABS, PS, PC/ABS) | about 30–45 MPa |
| Engineering resins (PC, PA, POM, PBT) | about 35–60 MPa |
| Thin walls, long flow, filled grades | about 50–80 MPa |
For example, a 1.0 mm wall PC part with a long flow path should be estimated near the top of its range. Our guides to injection molding wall thickness and thin-wall injection molding explain why.
Key Takeaway: For this reason, choose pressure from wall and flow length, not from resin alone.
What Does a Clamping Force Calculation Example Look Like?
A clamping force calculation example shows how the inputs combine.
- Part: ABS cover, 80 × 50 mm, 2.0 mm wall.
- Projected area: 40 cm² per part.
- Cavities: 2, plus 8 cm² runner = 88 cm².
- Pressure: 40 MPa for ABS at 2 mm wall.
- Force: 88 × 40 ÷ 10 = 352 kN.
- Safety factor: × 1.15 = about 405 kN, about 41 tonnes.
- Press: choose a press of about 60–80 tonnes after checking tie bars, mold size and shot size.
For example, if the mold is too wide for a 60-tonne press’s tie-bar spacing, a larger press is needed even though the force fits. Our guide to estimating molding cycle time uses press size in costing.
Key Takeaway: Overall, the calculated force is the minimum; mold size often decides the final press.
Which Other Press Checks Follow the Calculation?
Other press checks follow the clamping force calculation before a machine is chosen.
- Tie-bar spacing larger than the mold width
- Minimum and maximum mold height
- Opening stroke for part removal
- Shot size: shot weight about 20–80% of barrel capacity
- Locating ring and nozzle radius match
- Ejector stroke and pattern
For example, a small three-plate mold may need extra opening stroke even though its clamp force is low. Our guide to mold base sizing explains these limits.
Key Takeaway: Equally, record the target press in the mold specification.
When Is Simulation Better Than Hand Calculation?
Simulation is better than a hand clamping force calculation when the margin is small or the part is complex.
- Thin walls or long flow paths
- Multi-cavity or family molds with uneven fill
- High-viscosity or filled resins
- Press near its limit
For example, Moldflow can show that peak clamp force occurs during packing and is 20% higher than the hand estimate. Our guide to mold flow analysis explains what simulation reports.
Key Takeaway: As a rule, simulate when the hand result is within about 20% of the press limit.
What Happens When Clamping Force Is Wrong?
Clamping force that is too low or too high causes different problems.
- Too low: flash at the parting line, mold opening, oversize parts
- Too high: vent crushing, burn marks, mold and press wear
- Wrong press: higher hourly cost or unstable process
For example, flash that appears only at full pressure often means the press is undersized. Our guides to injection molding flash and plastic injection molding explain the process side.
Key Takeaway: Finally, set clamp force close to need, not to the press maximum.
FAQ
- Q: How do you calculate clamping force?
- Multiply projected area by cavity pressure and a safety factor of about 1.1–1.2.
- Q: What cavity pressure should I use?
- About 20–80 MPa depending on resin, wall thickness and flow length.
- Q: What is projected area?
- The footprint of parts and runner in the mold opening direction.
- Q: How many tons per square inch for injection molding?
- Commonly about 2–5 tons per square inch for estimates.
- Q: Does clamp force affect flash?
- Yes, too little clamp force lets the mold open and flash.
Conclusion
Clamping force calculation uses projected area, cavity pressure and a safety factor to size the press. Choose pressure by resin, wall and flow, check tie bars, mold height and shot size, and simulate when the margin is small. To check press fit for your part, send your 3D model and 2D drawing to our engineers.